Triple Entry Custom Pet Carriers: 3 Access Points
A triple entry carrier is not a double entry carrier with one more zipper: adding a third access point adds roughly 1.9 metres of zipper run, 14 to 18 extra pattern pieces and about USD 2.40 to 4.10 to unit cost at 500 pieces. It is worth that money when the product needs a top opening for loading, a front opening for examination without unloading, and a side opening for cleaning and airflow.
Executive summary
Three openings turn a bag into a chassis problem. Every opening cuts the shell, and every cut removes structural continuity from a panel that was carrying load, so the design question is never "can we add another zipper" but "where does the load go once we cut". Answer that well and the third opening feels effortless; answer it badly and the carrier sags at the corners and the zips track badly within a month.
From a brand angle, three openings also triple the decisions about where the logo sits and which opening reads as the front of the product. We treat the top as the retail-facing mark, the front as the veterinary-facing function, and the side as the repeat-exposure surface. Commercials are stable across the range: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production 35-50 days after approval, and AQL 2.5 inspection on every shipment. Our production team builds and validates multi opening prototypes at an SGS-verified production base audited to BSCI and ISO 9001, with structural checkpoints logged against the management system described by the ISO 9001 quality management standard.
Personalized pet carrier work splits into two tracks: variable data such as a name, and fixed branding such as a woven label or patch.
What a Third Access Point Actually Buys the Owner
The first opening on any pet carrier exists because the animal has to go in. The second exists because somebody has to reach the animal. The third exists because of a specific, repeatable moment in ownership, and if you cannot name that moment the third opening is decoration and should be cut from the specification.
In our experience the three moments that justify it are these. A top opening handles loading, because most animals accept being lowered into a box far more readily than being pushed through a tunnel. A front opening handles contact: a veterinarian, a groomer or a border inspection officer can look in, touch a head and read a collar tag without the pet being lifted out and without the handler losing control. A side opening handles maintenance, because it is the panel a customer opens at home to swap a liner, wipe a corner, or let air cross the interior while the carrier sits on a seat.
That division of labour is the whole argument. A carrier with three openings on the same face is three versions of the same gesture and reads as indecision. A carrier with a top, a front and a side is three different answers to three different situations, and customers perceive that as thought rather than as feature inflation.
There is also a safety argument that is easy to overlook. Reaching into a carrier from the front, rather than lifting an anxious animal out through the top, removes the moment of maximum escape risk. That is the reason clinic-facing and airline-facing products converge on a front door, and it is the reason a third opening tends to appear first on products positioned for travel rather than on products positioned for the living room.
Finally, a third opening changes how the product photographs. A bag that opens in three directions has three configurations for a product page and three set-ups for a retail shelf, which is a quiet but real marketing dividend on a category where imagery does most of the selling.
One caveat belongs in the brief. A third opening lengthens the explanation a sales assistant has to give, and on a self-serve shelf that is a cost rather than a benefit. The feature sells best when the three openings are self-evident in the photograph: if a customer has to read the hangtag to understand what the third zipper is for, the design has not finished the job and the opening should either be made more obvious or removed.
Chassis Engineering: Where the Load Goes After You Cut
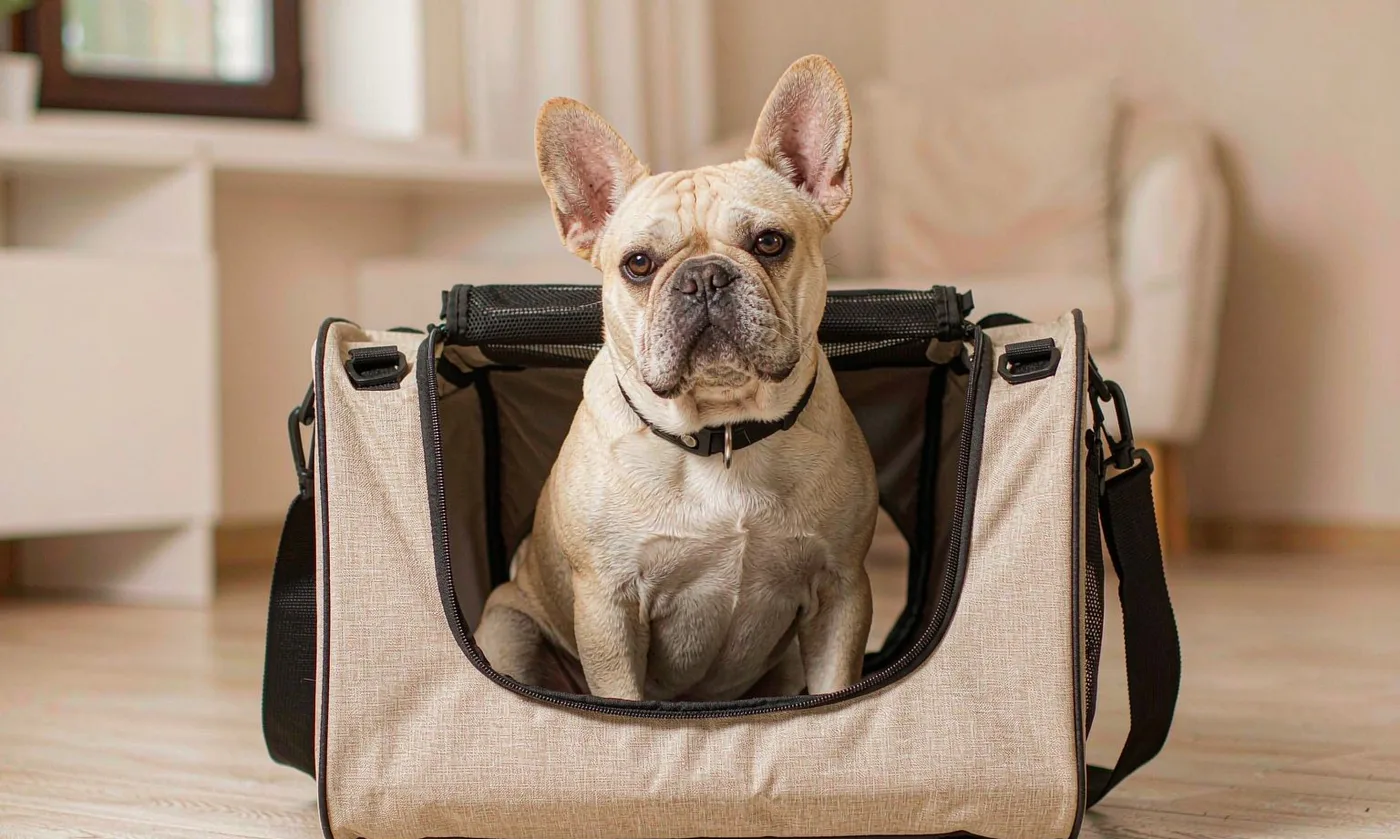
A soft carrier carries load through its shell. When the shell is continuous, tension from the handles distributes around the whole perimeter and the base takes compression. Cut a 60 centimetre zipper into that shell and you have removed 60 centimetres of load path; the tension now has to find another route, and it will find it through the weakest nearby seam unless you give it something better.
The standard solution is a continuous reinforcement path that bypasses the opening. On our multi opening builds that means a 25 millimetre webbing loop running from handle root to handle root through the base, stitched with a 3 to 4 stitch-per-centimetre box pattern at each termination, so the handle load never travels through the zipper tape. The zipper then only has to keep the panel closed, which is a much easier job than holding the bag together.
The second decision is the baseboard. A single opening carrier can get away with a 4 millimetre board floating in a sleeve. Once there are three openings, the shell above the base is no longer stiff enough to hold the box shape, so the board has to do more work: we move to a 5 to 6 millimetre laminated board with a perimeter binding, or to a moulded tray with a 12 to 18 millimetre wall where the product has to hold shape empty on a shelf.
Corner behaviour is where weak triple entry designs fail first. Each opening terminates near a corner, and three terminations in the same corner concentrate every stress in one 40 millimetre square. The fix is to stagger the terminations so no two openings end within 60 millimetres of each other, and to run a reinforcement patch behind each termination that is larger than the zipper end by at least 20 millimetres in every direction.
Sag is the visible symptom. A three opening carrier that has not been reinforced properly measures 8 to 15 millimetres narrower at the top than at the base after two weeks of display, and that taper is immediately legible as cheapness on a shelf next to a product that holds its line.
Panel Count, Seam Length and the Real Cost Delta
Cost in this category tracks two numbers: metres of zipper and minutes of sewing. Both climb sharply with the third opening, and both should be modelled before the design is committed rather than discovered in costing.
A two opening carrier typically carries 3.4 to 4.0 metres of zipper. Adding a side door brings the total to 5.3 to 6.2 metres, and the extra length is not purely additive because each opening needs a start and a stop, a garage, a binding and a reinforcement patch. Sewing minutes move from roughly 22 to roughly 31 per unit, which at a fully loaded labour rate is the single largest component of the increase.
| Configuration | Zipper run | Pattern pieces | Sewing minutes | Unit cost delta |
|---|---|---|---|---|
| Single top opening | 2.1 m | 9 | 17 | baseline |
| Two openings (top + front) | 3.7 m | 13 | 22 | + USD 1.30 to 2.20 |
| Three openings (top + front + side) | 5.8 m | 18 | 31 | + USD 2.40 to 4.10 |
| Three openings with moulded base tray | 5.8 m | 21 | 34 | + USD 4.60 to 6.80 |
Those deltas are why the third opening belongs on products with a price ceiling that can absorb it. On a program targeting USD 19 retail, a four dollar increase in landed cost is fatal. On a program targeting USD 79, it is invisible and it buys a feature that competitors at that price will not have.
Pattern piece count matters to the brand owner for a second reason. Every additional piece is another opportunity for a colour mismatch between panels, and on a multi colourway program that risk multiplies. We standardise panel suppliers within a colourway precisely to keep the third opening from introducing shading across the shell.
Where the money is usually recovered
There is almost always 1.50 to 2.50 dollars of recoverable cost in a triple entry specification. The most common sources are an oversized reinforcement patch, a heavier zipper gauge than the panel requires, and a moulded tray specified where a laminated board would hold shape adequately. Trimming those three items rarely shows in the finished product and reliably shows in the costing sheet.
Zipper Architecture for the Third Opening
The third opening is usually the one that gets the least engineering attention and therefore the one that fails first. It is typically the side door, it is typically curved, and it is typically the opening a customer uses while the carrier is on a surface rather than in the air, which means it is operated with the shell under compression. A zipper that runs beautifully on a bench can bind badly when the bag is loaded and sitting on its side.
Gauge selection is the first decision. A number 5 coil is adequate for a side door under 45 centimetres; above that we move to a number 8, because the longer the run the more the tape stretches under load and the more the slider has to fight. Chain type is the second: reverse coil hides the teeth and gives a cleaner exterior line, which matters on a panel that is facing the customer in a product photograph, while a standard coil is slightly cheaper and slightly easier to repair.
Termination design deserves more attention than it usually gets. Every zipper end needs a garage, a small fabric pocket the slider parks in, and the garage needs to be deep enough that the slider body is fully enclosed. On a side door the garage should sit at the top of the run, not the bottom, so gravity and vibration do not work the slider toward the opening. We also specify a second, smaller pull tab on the interior side of the front door so the handler can open it from inside without releasing the outer zipper fully.
Puller choice is where the brand shows up most cheaply. A custom puller with a moulded logo costs a fraction of a metal badge and gets touched on every single use, which is arguably the highest frequency brand contact on the entire product. We recommend a 45 to 60 millimetre puller body on the front door, a smaller one on the side, and a plain matching puller on the top so the hierarchy reads as deliberate.
Hardware specification for a door that is used daily
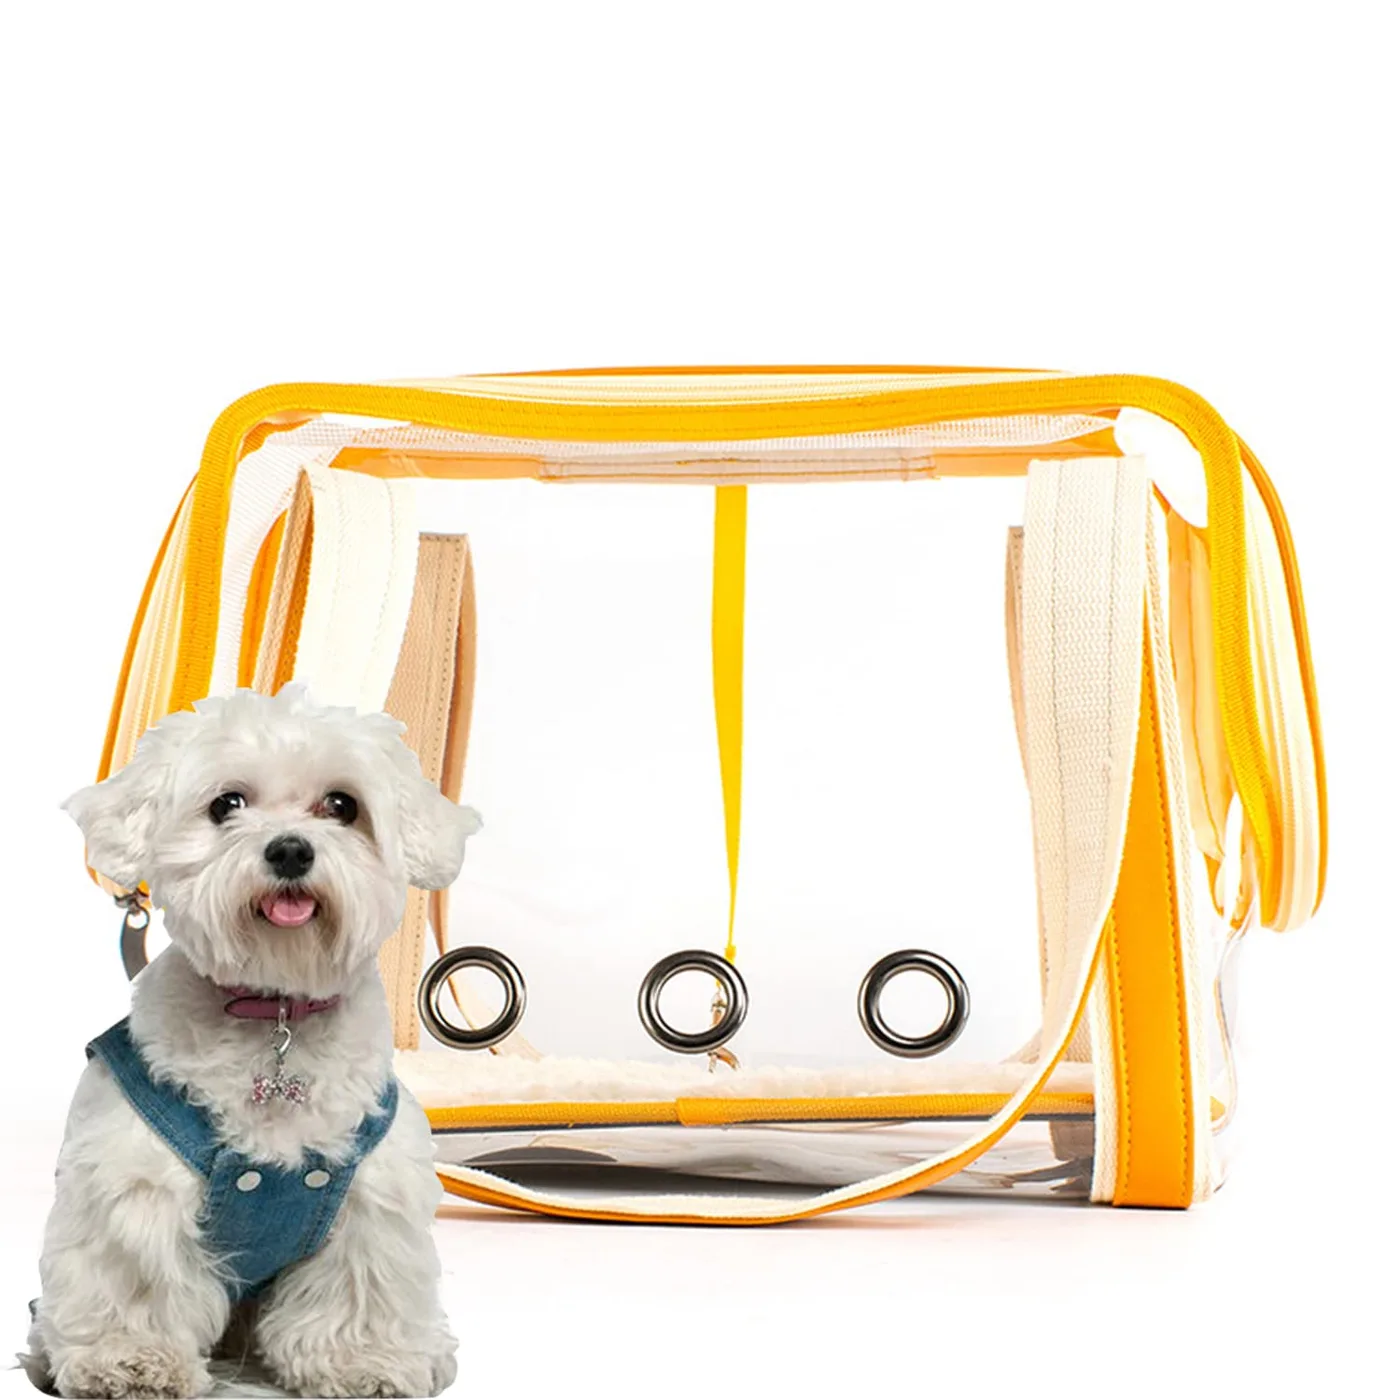
The side door is opened more often than any other opening on the product, so its hardware should be specified one grade above what the panel seems to need. We use a metal slider body rather than a cast one on runs over 50 centimetres, a slider with a locking pin where the door is curved, and a puller attached through a 4 millimetre grommet rather than through the tape itself, because tape attachment is the most common point of puller failure.
Tape colour deserves a decision too. A matched tape disappears into the shell and reads as design; a contrast tape reads as utility. On a premium program we match, and we reserve contrast tape for the opening we want the customer to find first, which is usually the front.
Brand Placement Across Three Openings
Three openings create three front panels, and a brand that puts the same logo on all three looks unsure which one matters. The fix is a placement hierarchy, and it should be decided before the pattern is cut because the reinforcement that each opening needs will constrain where a mark can sit.
Our default hierarchy is simple. The top panel carries the primary mark because it is the surface facing the camera in a hero shot and facing the aisle on a shelf. The front panel carries a small secondary mark, offset to one side of the opening so the zipper does not cut through it. The side panel carries no mark at all, or a woven tab at most, because it is the surface that gets handled and scuffed.
Decoration method should follow the surface. The top panel, which is usually the flattest and most stable, will take an embroidery or a debossed patch. The front panel flexes, so a heat transfer or a silicone badge behaves better than a rigid mark. The side panel is the natural home for a woven label, because a tab at a seam reads as a detail rather than an advertisement and survives abrasion better than a print.
Colour is the other half of the decision. On a dark shell, a tonal mark on the side and a contrast mark on the top creates depth without noise. On a light shell the reverse applies, and we generally recommend that the side mark be tonal regardless, because that panel will be handled more than any other and a tonal mark hides wear better.
One discipline pays off across the whole program: standardise the logo size ratios between panels and write them into the tech pack. A brand that specifies "logo centred on each panel" will receive samples with three different visual weights, and reconciling them after sampling is one of the most common sources of delay we see.
Placement rules we apply by default
Marks stay at least 25 millimetres clear of any zipper tape. No mark crosses a seam. No mark sits within 40 millimetres of a handle root, where the fabric folds under load. Primary and secondary marks differ in size by a factor of roughly 2.5, and every mark is positioned against the closed configuration, not the flat pattern.
Airflow, Visibility and the Comfort Argument
Three openings is also a ventilation strategy. A carrier with a single top door tends to be a still-air box: warm air rises and has nowhere to go, and the animal sits in the warmest stratum. Open a front and a side panel and you create a cross-flow path, which on a warm day is the difference between a pet that settles and a pet that pants.
The design target we work to is a mesh area of at least 22 percent of the total shell surface, distributed on at least two non-adjacent faces. That second condition is the important one: mesh on two adjacent panels still leaves a stagnant corner, whereas mesh on opposing or perpendicular panels gives a real path. Aperture size follows the animal: a 1.5 millimetre aperture resists claw penetration on small breeds, while a 3 millimetre aperture moves substantially more air on a large breed where claw capture is less of a concern.
Visibility is the comfort argument that customers actually articulate. A pet that can see its owner through a front panel settles faster than one sealed into a soft box, and the owner can check on the animal without opening anything. That is why we favour a front panel with a mesh window protected by a fabric flap: closed, it gives privacy in a busy terminal; open, it gives the animal a sightline.
There is a testing dimension. Airflow claims are easy to make and hard to defend, so we log measured open area as a percentage of shell surface in the tech pack and verify it against the retained sample at inspection. Where a program targets travel retail, we also reference the carrier guidance published by the Center for Pet Safety when framing ventilation and restraint expectations with buyers.
Sightline height and panel position
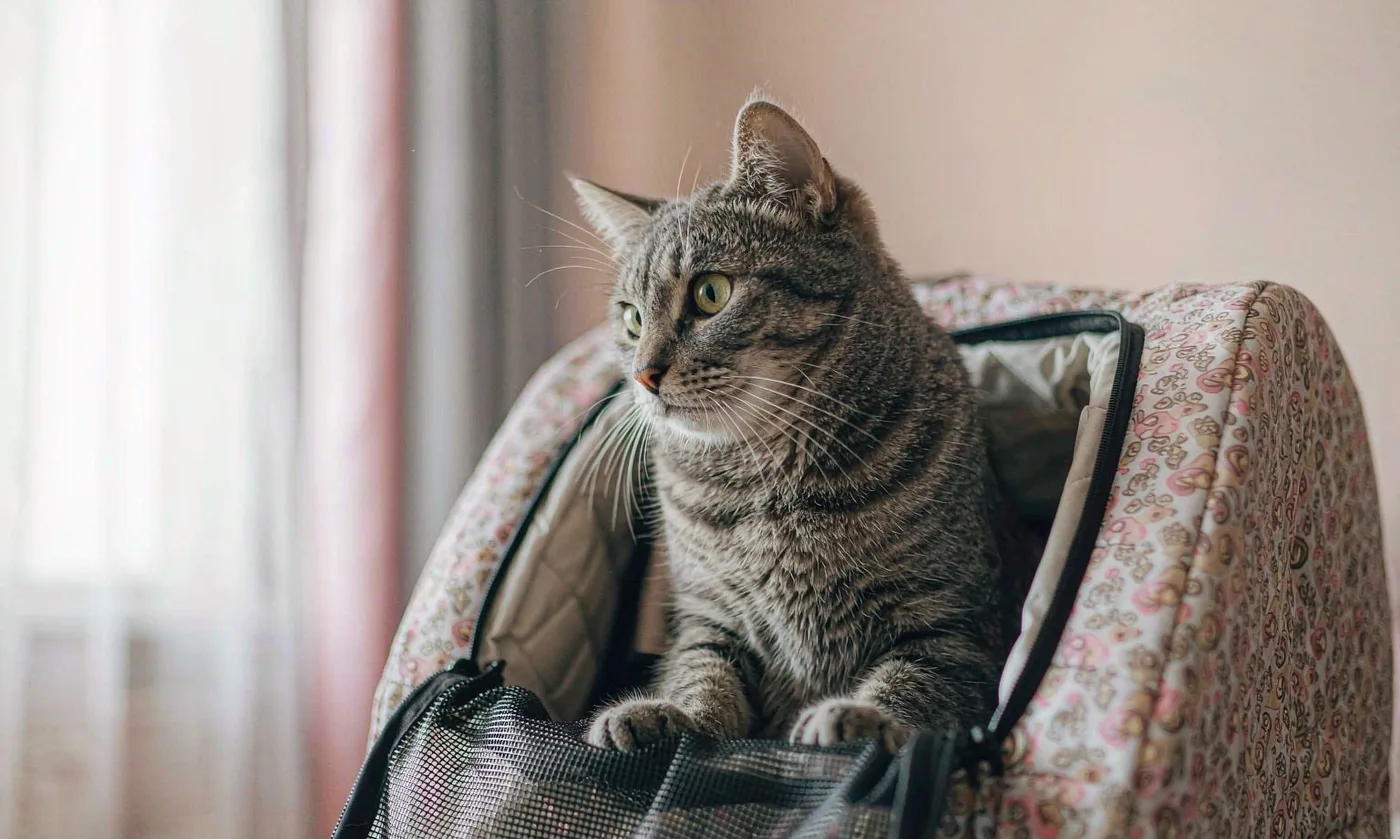
A mesh window positioned below the animal's eye line when lying down gives the owner a view of a back rather than a face. We set the lower edge of the front window at 40 to 55 percent of interior height, which puts the sightline at or just above the head of a lying animal for most small and medium breeds.
Lining and colourway coordination across three doors
Three openings means three interior views of the lining, and the lining is where a cheap program is exposed. We specify one lining colour per colourway rather than one per panel, and we require the lining to be cut from the same dye lot across the whole order, because three separate panels in three slightly different shades is the kind of inconsistency a retailer notices immediately and a spec sheet never captures.
Where the program uses a printed lining, the repeat has to be planned against the openings. A motif that lands behind a zipper reads as a mistake, so we place the repeat origin at the centre of the front door and let it fall where it falls elsewhere. It is a small discipline that removes an entire class of sampling revision.
Sampling and Validation Before Bulk
A triple entry prototype has to be tested in the configurations it will actually be used in, which is more configurations than most teams bother with. We sample three: empty on a shelf, loaded on a seat, and loaded and lifted by one handle while one opening is unzipped. The third is the one that exposes chassis problems, because it is the moment when the reinforcement path is carrying everything and the shell is doing nothing.
The zipper cycle test is the second gate. Each opening is cycled 500 times on a fixture with the shell under a representative load, and we record slider force at the start and at the end. A jump of more than 25 percent in required pull force predicts field complaints about a zipper that "gets stiff", and it usually traces back to tape stretch from an under-specified gauge.
Sag measurement closes the structural loop. We measure top width and base width on the retained sample, then repeat after a 72 hour loaded display period. Any taper beyond 5 millimetres sends the pattern back for reinforcement, not for a heavier fabric; heavier fabric treats the symptom and adds cost, whereas reinforcement treats the cause.
Commercials stay constant through this process: samples in 6-10 working days per iteration, bulk 35-50 days after final approval, MOQ 500 pieces per colourway, and every shipment inspected to AQL 2.5 against the retained approved sample. Where a program needs a moulded tray or a custom puller, the tooling is quoted separately and adds roughly two weeks to the first article date, which is the single most common schedule surprise in this configuration.
If you are deciding between a two and a three opening architecture, the comparison with our dual entry carrier program is the natural next read, and the single-access baseline is covered in detail in the top entry design note.
Why brands source here
- Pet carrier programs run since 2014; founding team in sewn goods since 2004
- SGS-verified production floor of 4,950 m² with 137 workers across 7 lines
- Monthly capacity of 200,000 units, audited to BSCI and ISO 9001
People Also Ask
Why do pet carriers have three openings?
Because loading, contact and cleaning are three different gestures. A top opening takes the pet in, a front opening lets a vet or handler reach it, and a side opening handles liners and airflow.
Is a triple entry carrier worth the extra cost?
Yes above roughly USD 59 retail, where the USD 2.40 to 4.10 cost increase disappears into the price and the feature differentiates the product. Below USD 19 retail it is rarely justified.
How is a triple entry carrier reinforced?
With a continuous webbing load path bypassing the openings, a stiffer baseboard, staggered zipper terminations and reinforcement patches behind each termination.
Which opening is safest for handling an anxious pet?
The front. Reaching in from the front removes the lift-out moment that carries the highest escape risk.
Can a triple entry carrier be used on an aircraft?
Most designs can, provided all openings close securely and the shell holds its shape under a seat. Check the specific airline before travel.
How much ventilation does a three opening carrier give?
Around 22 to 30 percent open area when two panels carry mesh, which is enough for a genuine cross-flow rather than trapped warm air.
Frequently Asked Questions
Does a third opening weaken the carrier?
Not if the load path is rerouted. A continuous webbing loop from handle root to handle root through the base carries the handle load, so the zipper only closes the panel rather than holding the bag together.
Which three openings do you recommend?
Top for loading, front for contact and examination, side for cleaning and cross ventilation. Three openings on the same face do not add function.
How much does the third opening add to unit cost?
Typically USD 2.40 to 4.10 at 500 pieces, driven mainly by the extra 2 metres of zipper and roughly 9 additional sewing minutes per unit.
Can each opening use a different zipper gauge?
Yes, and it is often correct. A number 5 coil suits a side door under 45 centimetres; longer runs and curved runs justify a number 8.
Will three openings affect airline acceptance?
It can help. A front opening allows inspection without removing the animal, which is what handlers prefer, provided the openings close fully and the shell holds shape.
How do you stop corner sag?
By staggering the zipper terminations so no two end within 60 millimetres, and by backing each termination with a reinforcement patch 20 millimetres larger than the zipper end on every side.
Can the side opening be mesh only?
Yes. A mesh-only side panel with a fabric flap is a common travel specification and costs less than a zippered side door.
What mesh area do you target?
At least 22 percent of shell surface, distributed across two non-adjacent faces so air has a genuine cross-flow path rather than a stagnant corner.
Can I put a different logo on each opening?
You can, but a hierarchy reads better: primary mark on the top, small secondary on the front, woven tab or nothing on the side.
Does the third opening change the MOQ?
No. The MOQ stays at 500 pieces per colourway. What changes is unit cost, sewing time and, if tooling is needed, the first article date.
How many sample iterations should I budget for?
Two is typical. The first resolves chassis and zipper behaviour, the second resolves logo placement and colour, at 6-10 working days per iteration.
Can openings be added to an existing pattern?
Rarely cleanly. Adding an opening to a pattern designed for two means re-engineering the reinforcement path, so we usually treat it as a new pattern.
Talk to QUANZHOU JUNYUAN BAGS about a pet carrier program: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample