D-Ring Attachment Point: A Custom Pet Carrier Hardware Guide
A D-ring attachment point is the metal loop that anchors a leash, shoulder strap or accessory clip to a custom pet carrier, and it should be specified by wire diameter, internal clearance and finish rather than by a catalogue photo. For a private label programme the working spec is a 3.0-4.0 mm welded ring with 25-32 mm internal clearance, a fully closed weld and a finish rated to 48 hours of neutral salt spray. Lock those three numbers and the ring stops being the weakest part of the bag.
Hardware is the fastest way to make a private label pet carrier look expensive, and the D-ring sits at the centre of that decision because it is the one metal part the customer touches every single day. This guide is written for brand owners and designers who are building an OEM or ODM line and want the attachment point treated as a design element rather than a commodity.
Our production team runs every custom programme on the same commercial cadence: MOQ 500 units per colourway, samples in 6-10 working days, bulk production in 35-50 days after written sample approval, and incoming hardware inspection at AQL 2.5. Standard terms are T/T 30/70 against FOB Xiamen, with test reports from an SGS-verified production base covering coating thickness, salt spray and static pull. Every figure quoted below is drawn from that working range so you can move from mood board to purchase order without pausing to re-quote. Hardware drawings are issued with body, finish and tape references on one sheet, so a re-order repeats the approved build instead of a remembered description of it. Test reports are filed against the lot number rather than the quotation, which is what makes a later claim answerable.
A personalized pet carrier programme needs the artwork file and the variable data list locked before sampling, otherwise the first shipment slips a full cycle.
Why the D-Ring Decides Whether a Custom Pet Carrier Reads as Designed or Merely Assembled
Ask a shopper why one pet carrier looks considered and another looks cheap and they will rarely mention the fabric first. They will mention weight, balance and the small metal details that catch the light. The D-ring is the most visible of those details because it lives on the outside of the silhouette, usually at the point where the eye lands after the logo. A thin, bright, rattling ring makes an otherwise well-cut shell feel like a sample; a solid, quiet, correctly toned ring makes a mid-priced shell feel like a considered product.
From a brand consultancy angle, the D-ring is doing three jobs at once. Structurally it transfers load from the strap or leash into the shell. Visually it sets the metal temperature of the whole bag, which then dictates what colour zip teeth, logo badge and webbing end caps you can use. Commercially it is the part most likely to appear in a returns photograph, because it is the part a customer pulls, twists and clips under real load.
That triple role is why we treat hardware selection as a design meeting, not a purchasing afterthought. When you brief a custom pet carrier programme, the attachment point should arrive with a drawing, a finish code and a test target attached to it, exactly as the fabric does. Anything less and you have handed the most visible metal on the bag to whoever happens to have stock that week.
There is also a storytelling dividend. A shape that belongs to your brand alone is defensible in a way that fabric colour is not, and it photographs well on a product page where the hardware sits against a plain background. Small metal, large return.
The commercial cost of a poor choice is measurable. Hardware appears in a disproportionate share of negative reviews for pet carriers because it is the part that fails in a way a customer can see and describe. A bent ring, a chipped coating or a rattle that develops after a month will be photographed and posted, while a well-executed ring will never be mentioned at all. Designing for silence and permanence is therefore not an aesthetic indulgence; it is a review-management strategy that costs a few cents per unit.
Alloy and Finish Options: Reading a D-Ring Spec Sheet Like a Designer
Four material families cover almost every private label brief, and each one changes both the bill of materials and the visual language of the collection. Zinc alloy die-cast gives you complex shapes and crisp edges at a low unit price, which suits fashion-led lines where the ring is sculptural. Welded carbon steel wire gives the cleanest classic silhouette and the highest strength-to-cost ratio. 304 stainless is the quiet premium answer for brands that promise corrosion resistance near salt water. Anodised aluminium is the lightest option and the only one that takes saturated colour properly.
Finish matters as much as substrate. Nickel-free plating is now the default requirement for anything sold into the EU or through retailers with restricted substance lists, and the chemistry has to be declared rather than implied. Powder coating hides die-cast porosity and gives a soft matte hand that reads well against technical nylon. Physical vapour deposition gives a harder, darker surface that resists the scuffing seen on black hardware after a season of use. Brushed and antique finishes hide fingerprints, which is a genuine selling point on a dark shell.
| Option | Typical spec | Hand-feel and look | Cost index | Best for |
|---|---|---|---|---|
| Zinc alloy die-cast | 25 mm, 2.8 mm section, nickel-free plate | Sculptural, crisp edges, heavier for its size | 1.0 | Fashion-led private label lines |
| Welded carbon steel | 3.5 mm wire, powder coat | Classic round profile, matte grip | 1.2 | Outdoor and utility collections |
| 304 stainless | 4.0 mm wire, brushed or mirror | Cool, dense, age-resistant | 2.1 | Coastal and premium programmes |
| Anodised aluminium | 3.0 mm section, colour anodise | Light, saturated colour, warm to touch | 1.8 | Colour-led capsule drops |
When you specify, ask for coating thickness in microns rather than a vague phrase such as heavy plating, and ask for the salt spray hours the finish has actually been tested to. Those two numbers are what separate a ring that looks right on day one from one that still looks right after a winter of wet pavements.
Compliance intersects here as well. Nickel release and certain coating chemistries fall under European chemical rules, and the practical way to evidence that is a test report tied to the specific finish code you ordered. Guidance on restricted substances is published by ECHA, the European chemicals agency, and referring to it in your tech pack keeps the conversation factual rather than adversarial.
A plating line also has a memory. Once a vendor has run a finish for you, the recipe, the bath chemistry and the rack position are recorded, and re-ordering becomes a matter of repeating a code rather than renegotiating a look. That institutional memory is worth protecting, which is another argument for changing hardware finishes rarely and deliberately rather than season by season.
Geometry, Wire Diameter and Load Paths: The Three Numbers That Actually Matter
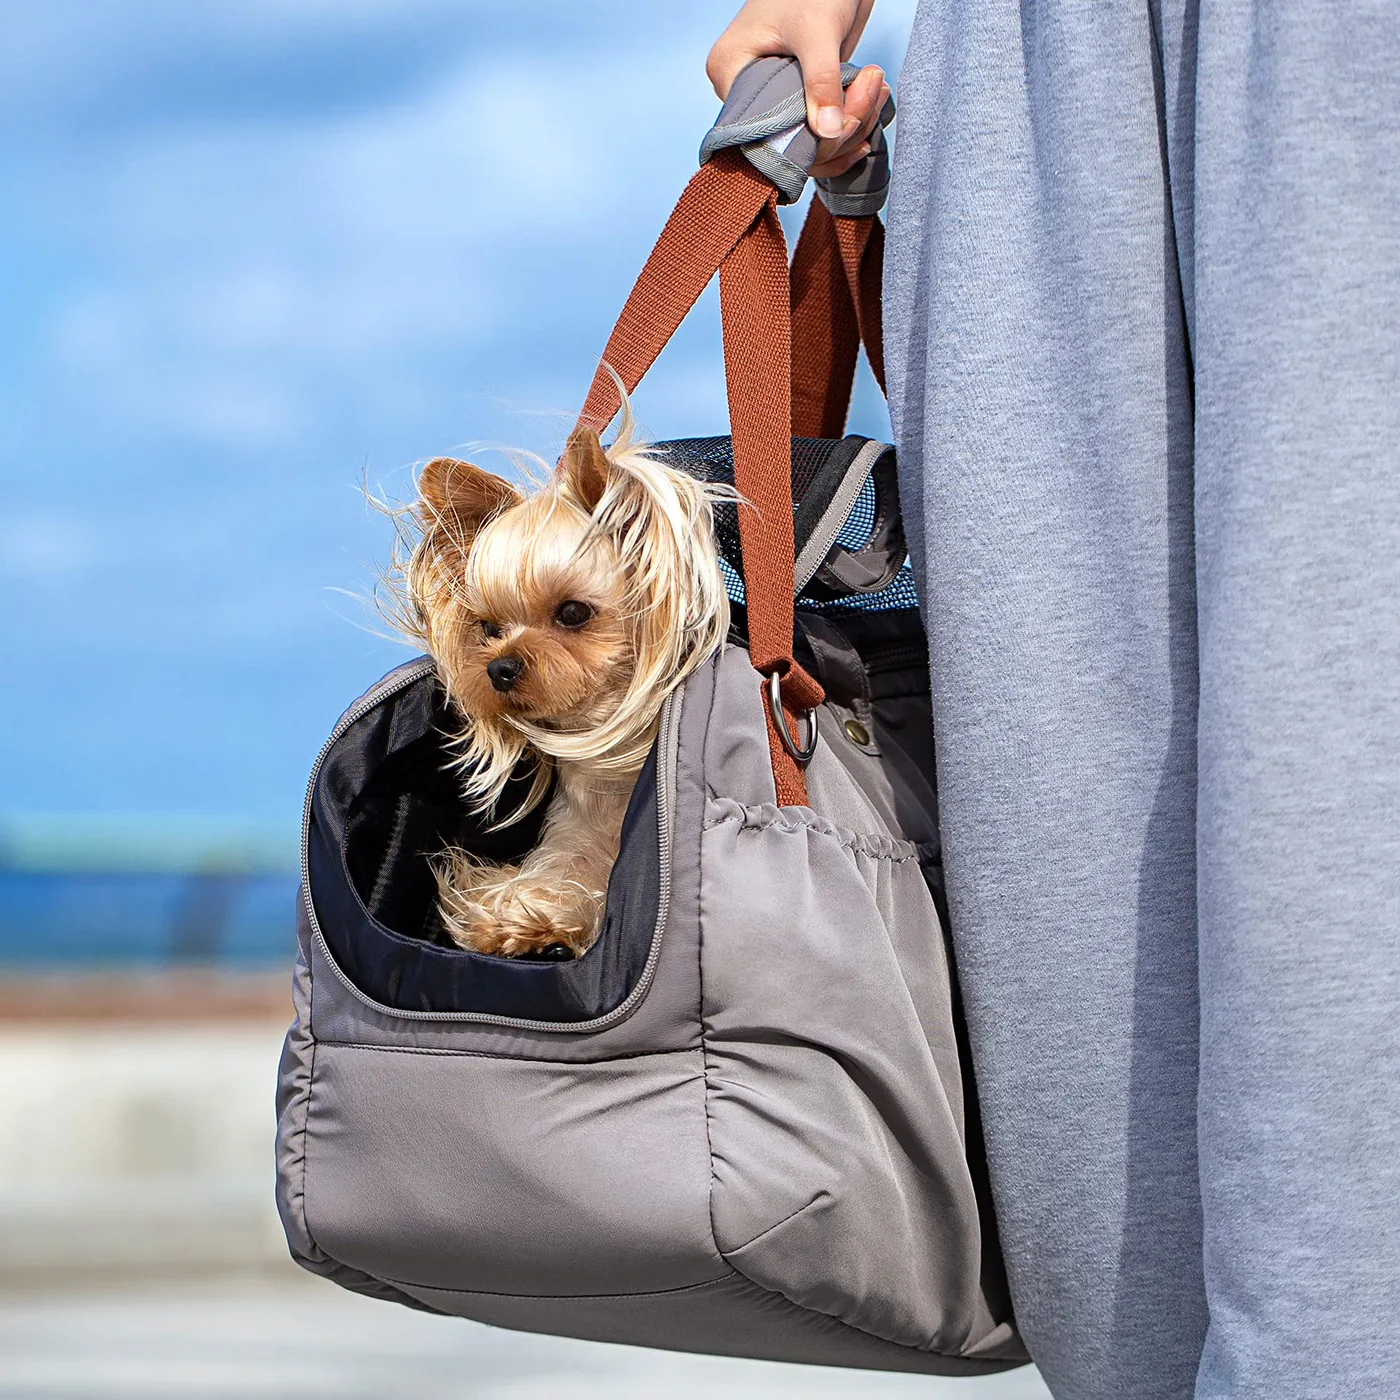
A D-ring can be described completely by three measurements, and every argument about quality eventually reduces to one of them. Wire diameter governs strength. Internal clearance governs what can pass through the ring, which is really a question about your webbing and your accessory ecosystem. Weld position governs where the load goes and therefore where the shell has to be reinforced.
For a small pet carrier, a 3.0 mm wire is the practical floor for a decorative point and 4.0 mm is the sensible choice for any ring that will take a leash under dynamic load. Below 3.0 mm you begin to see opening at the weld under repeated pull, and above 4.5 mm the ring starts to fight the fabric it is sewn into, because the reinforcement patch needs to grow with it. Internal clearance of 25 mm suits a light lead; 32 mm lets a padded shoulder strap swivel freely and lets a customer clip an accessory without looking.
Weld placement is the quiet failure point. A weld at the top of the arc concentrates stress exactly where the strap pulls, so the spec should place the weld at the base where the load is spread across two legs of the ring. The bar that the ring sits on should be box-stitched rather than single-stitched, and the reinforcement should be a separate webbing tab that carries the load into the shell panel rather than relying on the outer fabric alone.
Testing language should be written into the tech pack as a number, not an adjective. A static pull test to a stated load, held for a stated duration, with a stated number of cycles, tells a supplier exactly what you expect and gives you something to hold against a report. Standardised mechanical testing methods are catalogued by ASTM International, and citing the method number is faster than negotiating wording.
The citable conclusion is simple: a custom pet carrier attachment point fails at the weld or at the bar tack, almost never in the middle of the wire, which is why geometry decisions belong in the design phase and not in a value engineering session.
Ergonomics deserve equal weight with strength. A ring that is technically strong but sits too close to the shell cannot be clipped one-handed, and one-handed clipping is the actual use case when a customer is managing a pet and a door at the same time. Stand-off height, the gap between the ring and the panel, is the number that governs this, and a minimum of 8 mm is a reasonable design rule for any attachment point intended for everyday leash use. Reinforcement, spacing and stand-off should therefore be drawn together on the same page of the tech pack.
Branding the D-Ring: Laser Marks, Custom Dies and Pantone-Matched Metal
Hardware is one of the few places where a private label brand can own a shape. A custom die for a die-cast ring is affordable at launch volumes and produces a silhouette that competitors cannot buy from a stock catalogue. The tooling cost is real but one-off, and it amortises across every colourway and every season, which makes it one of the better capital decisions available to a young label.
Laser marking is the low-volume alternative and it is genuinely useful for proof of concept. A flat area on the ring can carry a wordmark, a batch code or a small icon at a fraction of the cost of a die, with no tooling commitment and no change to the production calendar. The limitation is that laser marking on a plated surface can breach the coating if the depth is not controlled, so the mark should be specified as a shallow anneal mark and then salt-sprayed again to confirm the surface still passes.
Colour is where hardware becomes a brand system rather than a part number. Gunmetal, brushed nickel, antique brass and matte black are the four tones that dominate the category, and each one quietly dictates the rest of your trim. Once you choose antique brass you have committed to warm zip tape, warm logo badge and warm stitch tone, and changing any of them later means re-shooting the whole line.
Anodised aluminium is the exception that allows saturated colour, and it should be managed with the same discipline as fabric. Reference the colour to a physical standard rather than a screen, and set a tolerance for batch-to-batch variation. Colour communication standards are maintained by Pantone, and naming the reference code in the tech pack removes the most common source of arguments about whether a sample matches.
There is a timing consideration as well. Custom dies and colour anodising both sit at the longer end of the sample calendar, so any brand planning a fixed-date launch should make the hardware decision before the fabric decision. Fabric can usually be substituted late with little schedule impact; a missing die cannot. Treating hardware as the critical-path item is the single most reliable way to protect a launch date in a custom pet carrier programme.
Cost Bands, MOQ Math and the Tooling Decision
Hardware economics reward early commitment. A stock ring bought at 500 pieces costs roughly what it costs at 5,000 pieces because the vendor is pulling from an existing run, whereas a custom ring carries a tooling charge that only makes sense once you know the shape will survive at least two seasons. The decision is therefore less about unit price and more about how confident you are in the silhouette.
Our commercial envelope is straightforward: MOQ 500 units per colourway on custom pet carrier programmes, samples in 6-10 working days, bulk production in 35-50 days after approval, inspection at AQL 2.5, T/T 30/70 and FOB Xiamen. Within that envelope, changing a ring from stock to custom typically adds tooling cost up front and moves the sample calendar by a week, but does not move the bulk window if the shape is signed off early.
| Route | Up-front cost | Unit cost effect | Sample time | Commitment |
|---|---|---|---|---|
| Stock ring, stock finish | None | Baseline | 6-8 working days | MOQ 500 per colour |
| Stock ring, custom finish | Low plate charge | +10 to 18 percent | 8-10 working days | MOQ 500 per colour |
| Custom die, standard finish | Tooling only | +15 to 30 percent | 10 working days | Tooling owned by brand |
| Custom die, matched anodise | Tooling plus colour setup | +30 to 55 percent | 10 working days | Two-season commitment advised |
The trap to avoid is customising hardware on the first drop before the silhouette has sold. A better sequence is to launch with a stock ring in a custom finish, prove the shape, then commission the die for the second season when volume justifies it and the risk has already been retired.
Freight and duty are easy to overlook in hardware costing because the parts are small. Metal hardware adds real weight to a shipment, and on a carrier that already has a rigid base and a padded strap, a move to stainless can add enough grams per unit to matter across a full container. Ask for the packed weight difference alongside the unit price difference and you will occasionally find that the cheaper metal is the more expensive decision once landed.
Sampling, Testing and AQL 2.5: How a D-Ring Spec Gets Locked
Sampling is where hardware specs are won or lost, because a ring is cheap to change on paper and expensive to change once five hundred shells are sewn. The working rhythm we recommend is a first sample built from stock parts to validate geometry and ergonomics, followed by a finish sample to validate colour and coating, followed by a golden sample that is signed off and retained on both sides.
Our production team works to samples in 6-10 working days and bulk in 35-50 days after written approval, and hardware is the item most likely to consume that window. Custom plating and custom dies sit at the long end; stock parts in a standard finish sit at the short end. If your launch date is fixed, book the hardware decision first and let the fabric follow it.
Inspection should be written into the purchase order rather than assumed. AQL 2.5 on incoming hardware covers appearance defects, coating flaws, dimensional checks against the drawing and a pull-test sample drawn from the same lot. Dimensional drift is the one that surprises brands, because a die wears over a long run and the ring that fitted the webbing in month one is a few tenths of a millimetre different by month six. Independent verification is available through SGS, and a report tied to a lot number is the cleanest way to close that risk.
Ask for three artefacts per delivery: a dimensional report against the drawing, a coating thickness reading, and a salt spray result with the hours stated. Three documents, one page each, and you have turned a subjective argument about quality into a checkable specification.
Retention matters more than paperwork. A signed golden sample held by both sides ends most disputes before they start, because the argument stops being about a written description and becomes a comparison against a physical object. Photograph the golden sample under neutral lighting, record the finish code and the lot number, and store both with the purchase order so that the next re-order can be matched to the same reference rather than to someone's recollection of it.
Building a Colour System Across a Six-SKU Collection
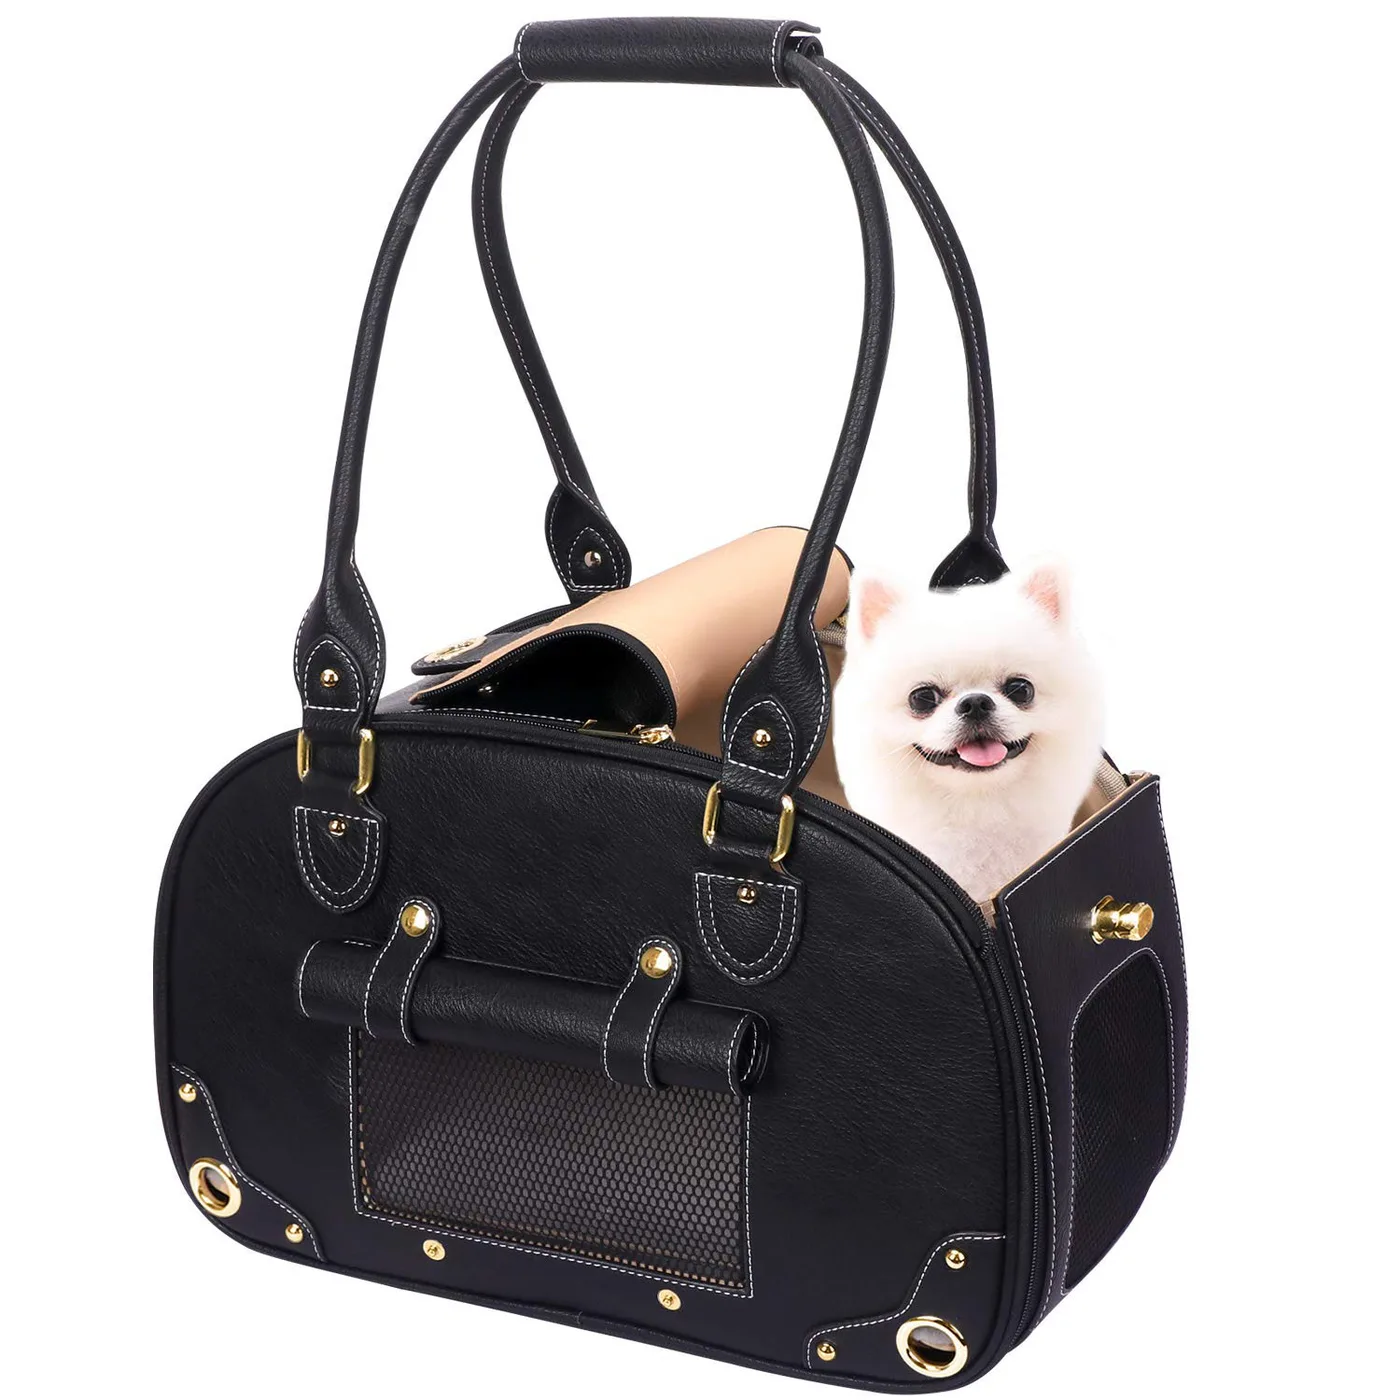
A single custom pet carrier is a product; six of them sharing a hardware language is a collection. The difference matters commercially because collections earn repeat purchase and single products do not, and hardware is the cheapest thread you can run through a range to make it cohere.
Start by fixing one metal tone for the core line and one accent tone for the capsule drops. The core tone should be the most forgiving finish available, which in practice means brushed or matte rather than mirror, because mirror shows every handling mark and every return photograph will show it too. The accent tone can be more expressive because it carries less volume and more margin.
Next, map the tone to the fabric palette and check the pairing under retail lighting, not daylight. Warm metals read brown under cool store light and cool metals read grey under warm store light, and the only way to catch that is to hold a physical card under the actual lighting. Send the card to your production team and reference the code, not a photograph.
Finally, write the tolerance. A stated acceptable range for batch-to-batch colour difference prevents both the rejection of acceptable goods and the acceptance of goods that will not sit next to last season's stock on a shelf. Textile colour measurement methods are published by AATCC, and borrowing their method numbers for your tech pack costs nothing and removes ambiguity.
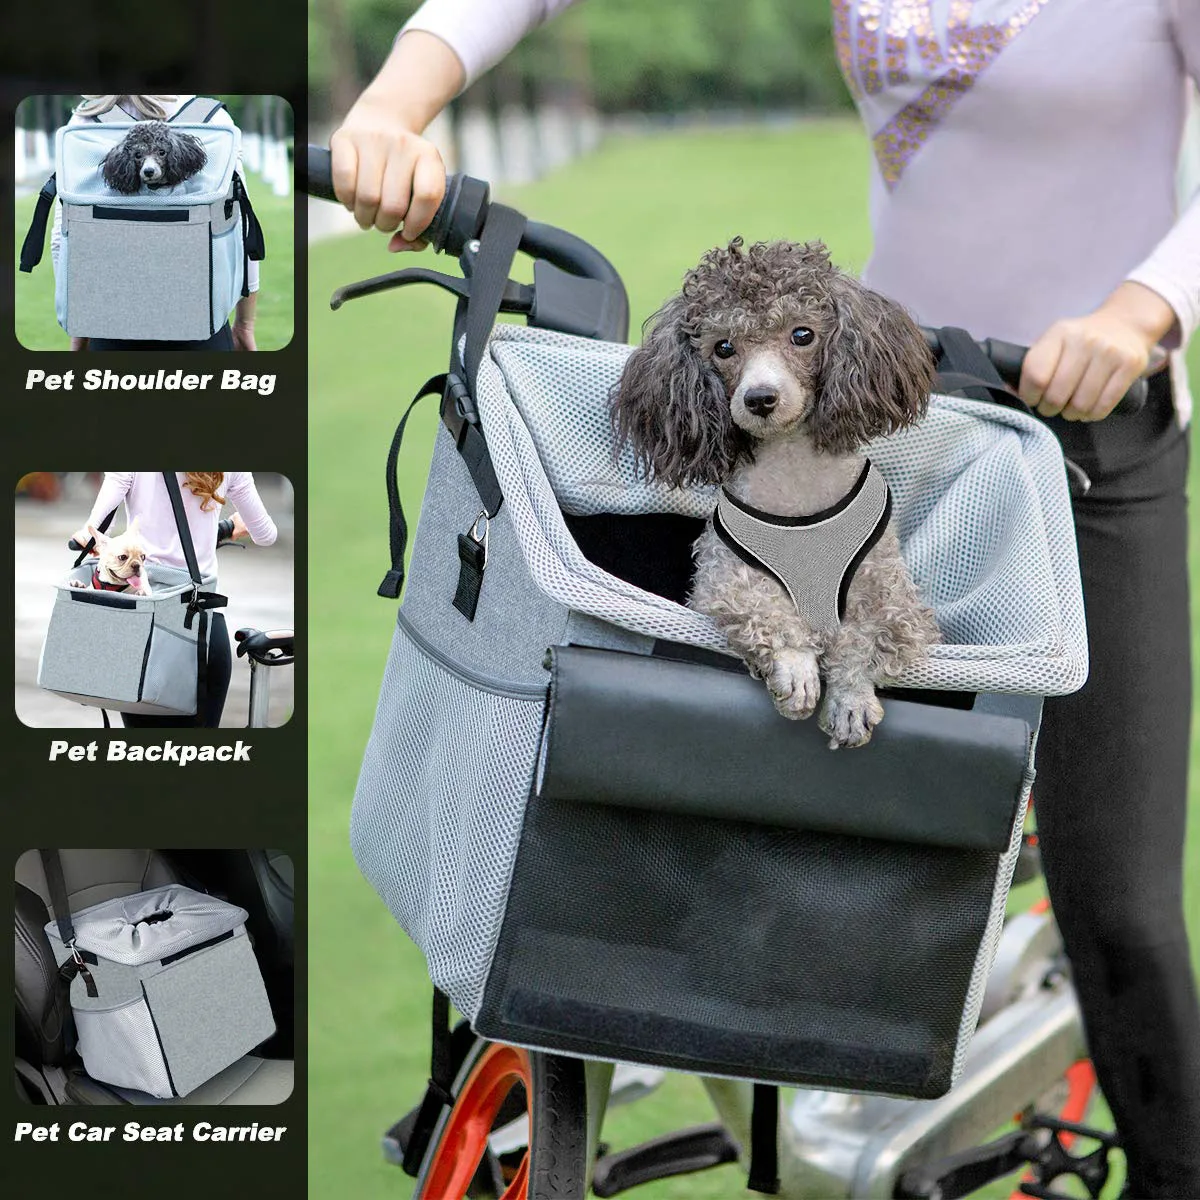
Accessory strategy is where a collection either compounds or fragments. If your attachment points accept a standard clip, you can sell a matching waste-bag holder, a treat pouch and a travel bowl that all fix to the same point, and every accessory sold reinforces the hardware language. Design the ring with that ecosystem in mind and the accessory line becomes a margin extension rather than a separate sourcing project.
Packaging, Presentation and the Unboxing Moment
Hardware-forward lines deserve packaging that lets the metal be seen. A ring buried in a sealed poly bag inside a dark box does no work for the brand; the same ring sitting on a header card with a short line about its finish does. The cheapest upgrade available to a young label is a printed card that names the hardware spec, because it converts a detail into a claim.
For ecommerce, the practical sequence is a protective sleeve on the metal to prevent scuffing in transit, a card that carries the finish name, and a box sized so the ring is not crushed against a corner. For retail, a counter display that puts one open carrier beside two folded ones lets the customer touch the metal without unsealing anything, which measurably reduces the number of opened boxes on a shop floor.
Instruction copy is part of the same design problem. A single line on the card telling the customer what load the attachment point is rated for does two things: it makes the product feel engineered, and it documents reasonable use in a way that is useful later. Keep the sentence short, keep the number honest, and print it where it will be read rather than filed.
Sustainability language belongs here too, but it must be specific. Naming the alloy and stating that it is recyclable is a claim you can support; saying the product is eco-friendly without a number is a claim that will eventually be challenged.
Finally, treat the hardware story as merchandising copy rather than technical copy. One sentence about the finish, one about the test and one about what the point attaches to is enough for a product page or a shelf card. Three short sentences beat a paragraph of specification, because the shopper scanning a page wants to know whether the metal will last, not how it was plated.
Production capability
- SGS-verified production space of 4,950 m², 149 machines, 7 assembly lines
- Pet carrier and pet bag output since 2014 from a 137-person team
- 200,000 units shipped monthly under BSCI and ISO 9001 systems
People Also Ask
How do you attach a D-ring to a bag?
The ring sits on a webbing tab that is box-stitched to the shell, with the reinforcement carrying load into the panel rather than the outer fabric.
What is a D-ring used for on a pet carrier?
It anchors a leash, shoulder strap or accessory clip and sets the visible metal tone of the whole product.
Are welded or seamless rings stronger?
Welded rings are standard and stronger than open designs, provided the weld is placed at the base of the arc where load is distributed.
How much weight can a D-ring hold?
It depends on wire diameter and weld quality, so specify a static pull test value in the tech pack rather than relying on a generic catalogue figure.
What is the MOQ for custom hardware on a pet carrier?
MOQ is 500 units per colourway, with samples in 6-10 working days and bulk in 35-50 days.
Can hardware be colour matched to my brand palette?
Yes, through anodising on aluminium or through finish selection on plated metals, referenced to a standard colour code.
Frequently Asked Questions
What wire diameter should a custom pet carrier D-ring use?
Use 3.0 mm as the minimum for decorative attachment points and 4.0 mm for any ring that takes a leash under dynamic load. Below 3.0 mm the weld tends to open under repeated pull.
What internal clearance do I need for a padded shoulder strap?
Specify 32 mm internal clearance. A 25 mm ring suits a light lead but constrains a padded strap and makes accessory clips awkward to attach.
Where should the weld sit on a D-ring?
At the base of the arc, where load is spread across both legs. A weld at the top of the arc concentrates stress exactly where the strap pulls.
Can I get a custom-shaped D-ring at launch volumes?
Yes, a custom die for a die-cast ring is affordable at MOQ 500 per colourway, but launch with a stock ring in a custom finish first and commission the die once the silhouette has proven itself.
Is nickel-free plating required?
For EU sales and most retailer restricted substance lists, yes. Declare the chemistry in the tech pack and request a test report tied to the specific finish code you ordered.
How long does a hardware sample take?
Samples run 6-10 working days. Stock parts in a standard finish sit at the short end; custom plating or a new die sits at the long end.
What is the bulk production window?
Bulk runs 35-50 days after written sample approval, on T/T 30/70 terms against FOB Xiamen.
What does AQL 2.5 cover on incoming hardware?
Appearance defects, coating flaws, dimensional checks against the drawing, and a pull test drawn from the same lot.
Can my logo be laser marked on a plated ring?
Yes, as a shallow anneal mark. Specify the depth and re-run salt spray afterwards to confirm the coating still passes.
Which finish hides fingerprints best?
Brushed or antique finishes. Mirror finishes show every handling mark and photograph badly in returns.
How do I keep hardware colour consistent between seasons?
Fix one core metal tone, reference a physical colour standard by code rather than a photograph, and write an acceptable batch-to-batch tolerance into the tech pack.
Does anodised aluminium allow brand colours?
Yes, it is the only family that takes saturated colour properly, which makes it the right choice for colour-led capsule drops.
Talk to QUANZHOU JUNYUAN BAGS about a pet carrier program: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample